

 english
 Русский
 Español
 Русский
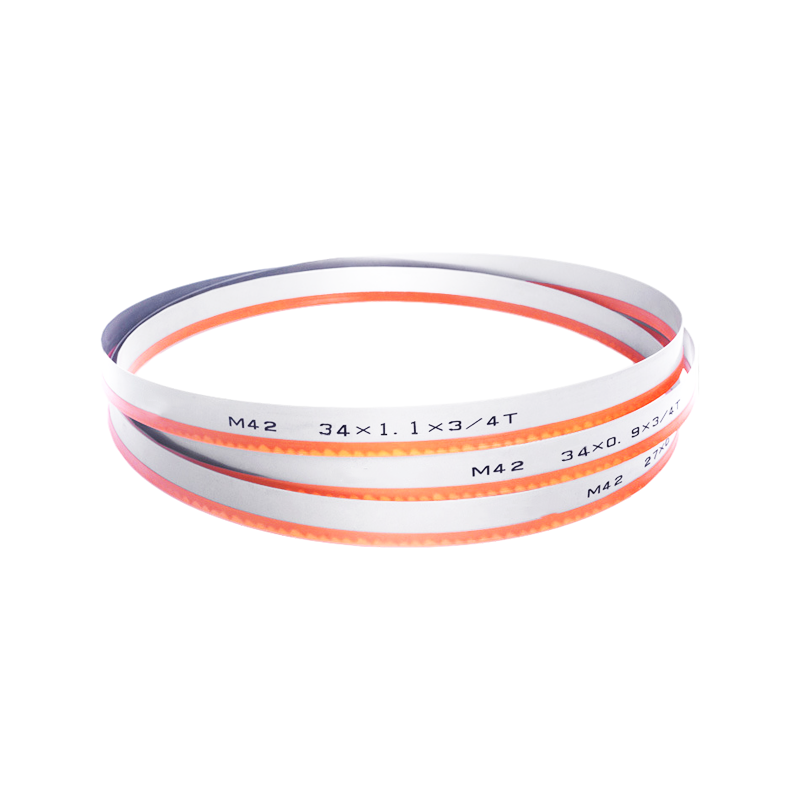
A band saw can have a sharp blade and still produce angled or inconsistent cuts. When the blade begins to wander, the problem may appear as poor squareness, uneven kerf width, premature tooth wear, or repeated adjustments on the machine. For production teams, replacing the blade immediately is not always the right solution. The workpiece, blade geometry, machine guides, tension, and cutting conditions should be considered together. A properly selected M42 Bi-metal band saw blade can support stable metal cutting, but its specification needs to match the actual application.
Start With the Cut, Not the Blade
When a cut is not straight, the should be to identify exactly where the deviation occurs. A blade that consistently moves away from the intended cutting line may indicate an unsuitable tooth configuration, incorrect blade dimensions, worn guides, or excessive operating pressure.
Engineers should compare the current cutting result with the original blade specification and inspect whether the problem appeared gradually or immediately after installation. This simple distinction can help separate normal blade wear from a machine or setup issue.
Blade Width Can Influence Stability
Blade dimensions are often selected according to the saw machine and application. A wider blade generally provides a different level of lateral support than a narrow blade, while blade thickness also affects flexibility and mechanical behavior.
This is why replacing a blade with a different width or thickness simply because the tooth pitch appears suitable can create unexpected results. Commercial M42 bi-metal ranges are offered in multiple widths, thicknesses, and tooth configurations for different metal-cutting applications.
For purchasing teams, the machine's original blade dimensions should be confirmed before evaluating alternative specifications.
Tooth Set Helps Create the Kerf
The teeth of a band saw are not positioned in a perfectly straight row. Tooth setting creates a kerf wider than the blade body, helping prevent the blade from binding in the workpiece. Different tooth forms and set patterns are used for different materials and cutting conditions.
When the tooth set becomes uneven through wear or damage, cutting behavior can change. This may result in wandering, rough surfaces, or increased resistance during the cut.
For this reason, tooth geometry should be evaluated as part of the complete blade design rather than treated as a simple TPI selection.
Check Machine Guides and Tension
A new blade cannot compensate for every machine condition. If the guides are worn, incorrectly positioned, or contaminated with chips, the blade may not remain properly supported during cutting. Incorrect blade tension can create another source of instability.
When investigating inaccurate cuts, production teams can review:
- Blade tension and installation
- Guide alignment and condition
- Wheel cleanliness
- Blade tracking
- Feed pressure
- Workpiece clamping
These checks are particularly important when the same cutting problem occurs with multiple blades.
Match Tooth Pitch to Material Thickness
Tooth pitch also has an influence on cutting stability because the number of teeth engaging the workpiece affects the cutting load. A pitch that is too coarse for a thin section may produce aggressive tooth engagement, while an unsuitable fine pitch can increase the number of teeth involved and affect chip clearance.
Industry selection guidance commonly recommends choosing TPI according to workpiece cross-section and material characteristics second. Variable-pitch configurations are also used for applications where changing engagement or vibration needs to be considered.
For mixed production, a manufacturer can help buyers establish separate blade specifications instead of forcing one blade to cover every material size.
Consider the Complete Cutting System
Straight cutting is the result of several factors working together. A blade with suitable M42 HSS teeth still needs the correct backing material, tooth geometry, dimensions, and machine setup. Current M42 bi-metal products are used across applications including structural sections, tubes, solid materials, and general steel cutting, with different blade designs available for different cutting requirements.
From a manufacturer's perspective, this is why application information is important during blade selection. Machine model, blade size, workpiece material, cross-section, and current cutting problems provide more useful information than simply requesting an M42 blade.
Make Straight Cutting a Purchasing Requirement
For industrial buyers, cutting accuracy should be part of the sourcing discussion rather than something evaluated only after delivery. A supplier should be able to discuss blade dimensions, tooth form, pitch, material construction, and application suitability before production.
When the blade is developed around the actual machine and workpiece, engineers have a clearer basis for testing and comparison. This also makes repeat purchasing easier because the approved specification can be linked to a specific cutting application.
A reliable M42 Bi-metal band saw blade is therefore not defined by the M42 designation alone. Straight cutting depends on the relationship between blade construction, tooth geometry, machine condition, and operating parameters. For manufacturers and distributors seeking consistent metal-cutting solutions, application-based specification remains a practical way to select an M42 Bi-metal band saw blade that supports accurate and repeatable production.
 CONTACT US

 CONTACT US